Key Points for Valve Installation
Sep. 29, 2026
Avoid These 5 Pitfalls in Valve Installation to Prevent 90% of Common Troubles
●Reversed flow direction: results in valve failure, internal leakage and seal damage.
●Misaligned flanges and disordered bolt tightening: causes biased pressure and leakage.
●Valve not fully open during welding: thermal deformation of sealing surfaces.
●Forced alignment: valve bears permanent stress, leading to cracking and leakage later.
●Installation without pressure testing and cleaning: foreign particles jam and damage sealing surfaces.
Pre-installation: Three Critical Checks to Eliminate Root Hazards
1.Verification of Documentation and Parameters
Verify that model, nominal diameter, pressure class, material and medium compatibility are 100% consistent with drawings.
Check certificates, pressure test reports and material certificates. Special service conditions (explosion-proof, high-temperature, corrosive) require specific certifications.
For safety valves, confirm intact lead seals; seals must not be removed without authorization.
2.Pre-inspection of Appearance and Performance
Valve body free of cracks, blowholes, deformation and corrosion; sealing surfaces scratch-free; flanges/threads undamaged.
Manually open and close the valve through full travel 2–3 times. No jamming or looseness; full open/close positions achieved.
For main pipeline valves and high-pressure valves, perform body strength test (1.5 times nominal pressure) plus seat leakage test. Installation permitted only after pressure holding without leakage.
3.Cleaning and Protection
Remove welding slag, rust and debris from valve cavity and pipe ends to prevent scratches on sealing surfaces.
Keep protective end caps on valves until installation. Store temporarily in dry and ventilated areas; place valve stem upward, do not stack, avoid outdoor rain exposure.
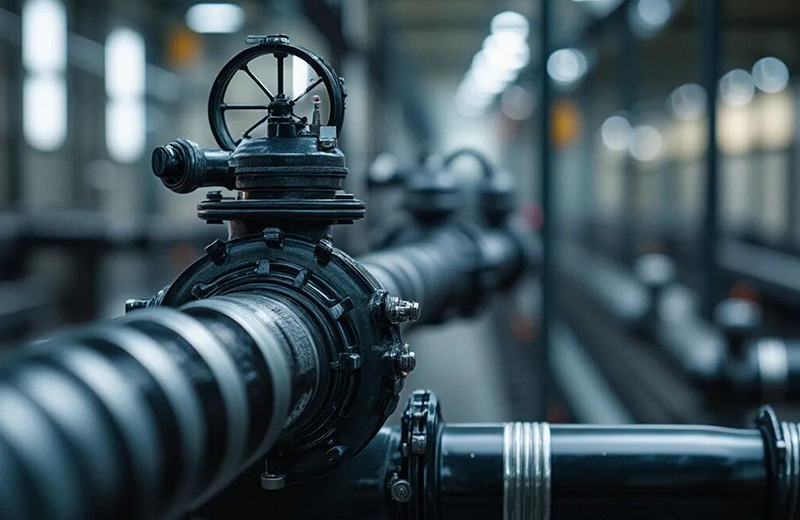
II. During Installation: Four Core Principles to Prevent Rework and Leakage
1.Flow Direction Must Not Be Reversed
Install in accordance with the arrow marked on valve body, matching the medium flow direction. Reverse installation is strictly prohibited.
Globe valves: medium enters from lower side and exits upper side. Reverse mounting leads to poor shut-off and excessive operating torque.
Check valves, steam traps and throttle valves: strictly follow flow direction and required mounting orientation (horizontal / vertical).
2.Location and Operating Clearance
Prioritize locations for easy operation, maintenance and inspection. Handwheel height is recommended at 1.2 m.
For valves on horizontal pipelines, handwheel shall not face downward. Install platforms or chain wheel operators for overhead valves.
Stagger adjacent valves, reserve ≥30 cm clearance for maintenance.
3.Connection Methods: Details Determine Sealing Integrity
◇Flange Connection (Most Common)
Install valve in closed position. Keep flange faces parallel and well centered; forced alignment is forbidden.
Place gasket centrally without offset. Tighten bolts diagonally in multiple passes with uniform torque.
High-temperature pipelines: cold pre-tightening plus secondary hot tightening to prevent high-temperature seizure.
◇Welded Connection
Carry out welding with valve fully open to protect sealing surfaces from deformation.
Use GTAW root pass, control welding temperature to avoid thermal stress damage to valve body.
◇Threaded Connection
Apply thread sealant / PTFE tape. Screw in by hand for 2–3 turns before final tightening; over-tightening is prohibited.
Leave 2–3 threads exposed. Clean excess sealant promptly to prevent entry into valve cavity.
4.Stress-free Installation Is a Bottom-line Requirement
Align pipes naturally; the valve shall not bear extra tension, torsion or weight from piping.
Install dedicated supports for large-bore and heavy-duty valves to avoid flange deformation and leakage.
III. Post-installation: Commissioning & Acceptance for Closed-loop Safety Control
Visual inspection: firm connections, correct orientation and clear markings.
Open/close test: smooth operation, correct position indication and no jamming.
Tightness test: conduct pressure test per specifications; no leakage at seats, packing and flanges.
Documentation filing: complete and traceable records of pressure test, commissioning and acceptance.
Quick Links
Quick Links
Contact Us
Phone : +86-510-8356 8681
Telephone : +86-139 2127 3425
E-mail : sales@xmzkf.com
Wechat : +86-139 2127 3425
WhatsApp : +86 139 2127 3425
Adress : No.6, Zhenyang Road, Yangshi, Luoshe Town, Wuxi, Jiangsu, China.